Tubewell Steel & Engg. Co. is a leading manufacturer and stockist specializing in Alloy Steel Pipes, Tubes, Fittings and Flanges for critical industrial applications.
9% Chromium – 1% Molybdenum – Vanadium creep-strength-enhanced forged fittings for supercritical and ultra-supercritical power plant piping.
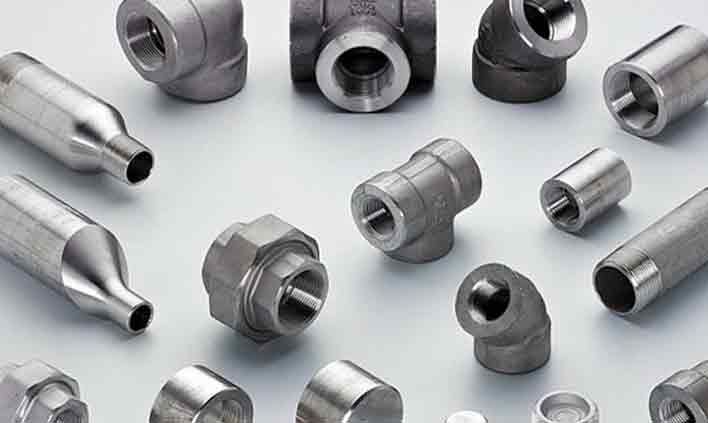
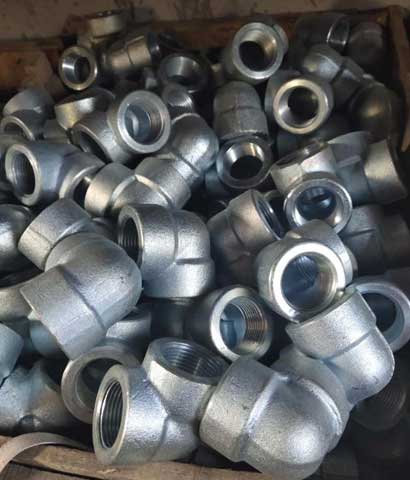
Tubewell Steel & Engg. Co. manufactures, stocks and supplies ASTM A182 F91 forged fittings in Mumbai, India. This vanadium- and niobium-modified 9Cr-1Mo grade offers exceptional creep strength and oxidation resistance, allowing thinner, lighter piping in supercritical boilers and high-energy steam systems.
The premium chrome-moly grade for supercritical service
ASTM A182 F91 is a modified 9% chromium – 1% molybdenum steel micro-alloyed with vanadium, niobium and nitrogen. These additions form fine, stable carbonitride precipitates within a tempered martensitic structure, giving creep-rupture strength far above F22 at temperatures up to about 650°C (1200°F). The result is fittings that tolerate higher steam pressures and temperatures with thinner walls and lower thermal stresses.
Because the properties of F91 depend on precise heat treatment, every fitting we supply is normalized at 1040–1080°C and tempered at 730–800°C as required by ASTM A182. Hardness is checked on 100% of pieces to confirm the 190–248 HBW range, and PMI confirms chromium, molybdenum and vanadium content. Fittings are supplied with EN 10204 3.1 certificates, IBR documentation and third-party inspection on request.
Standard supply range for ASTM A182 F91 forged fittings
| Parameter | Details |
|---|---|
| Material Standard | ASTM A182, ASME SA182 |
| Grade | F91 (UNS K90901), Type 1 / Type 2 |
| Dimension Standard | ASME B16.11, MSS SP-79, MSS SP-95, MSS SP-97, BS 3799 |
| Size Range | 1/8" NB to 4" NB |
| Socket Weld Class | Class 3000, 6000, 9000 |
| Threaded Class | Class 2000, 3000, 6000 |
| Thread Type | NPT (ASME B1.20.1), BSPT |
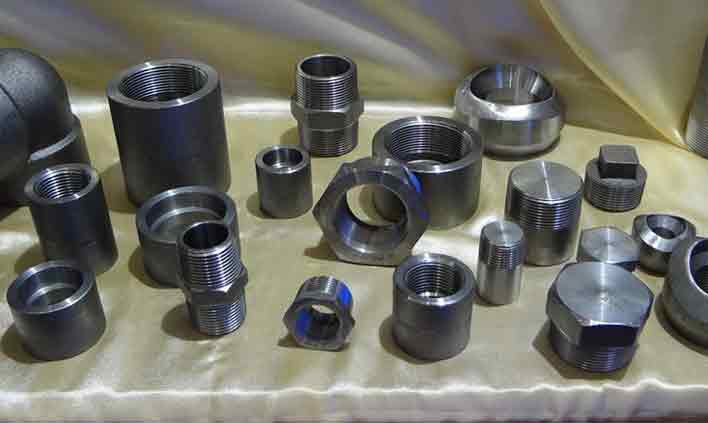
| Types | 90° & 45° Elbow, Tee, Cross, Full / Half Coupling, Cap, Boss, Plug, Swage Nipple, Sockolet, Weldolet |
| Manufacturing | Closed-die forged, CNC machined |
| Heat Treatment | Normalized 1040–1080°C & Tempered 730–800°C |
| Hardness | 190 – 248 HBW (100% checked) |
| Marking | As per MSS SP-25 – A182 F91, class, size, heat no. |
| Testing | Hardness, PMI, Tensile, Dimensional, Micro-structure, UT / DPT / MPI on request |
| Certificates | EN 10204 3.1 / 3.2, IBR Certificate, TPI Reports |
International equivalents of A182 F91
| Grade | ASTM | UNS | EN | W.Nr. | Nominal Alloy |
|---|---|---|---|---|---|
| F91 | A182 F91 | K90901 | X10CrMoVNb9-1 | 1.4903 | 9Cr – 1Mo – V – Nb |
Weight %, as per ASTM A182 (F91 Type 1)
| Grade | C | Mn | P | S | Si | Cr | Mo | Ni | V | Nb | N | Al |
|---|---|---|---|---|---|---|---|---|---|---|---|---|
| F91 | 0.08 – 0.12 | 0.30 – 0.60 | 0.020 max | 0.010 max | 0.20 – 0.50 | 8.0 – 9.5 | 0.85 – 1.05 | 0.40 max | 0.18 – 0.25 | 0.06 – 0.10 | 0.03 – 0.07 | 0.02 max |
Ti and Zr are restricted to 0.01% max each. F91 Type 2 (per current ASTM A182 editions) has tighter limits on residual elements and N/Al ratio.
Minimum values at room temperature as per ASTM A182
| Grade | Tensile Strength | Yield Strength (0.2%) | Elongation | Reduction of Area | Hardness (HBW) |
|---|---|---|---|---|---|
| F91 | 585 MPa (85 ksi) min | 415 MPa (60 ksi) min | 20% min | 40% min | 190 – 248 |
Typical values (for reference)
| Property | Metric | Imperial |
|---|---|---|
| Density | 7.76 g/cm³ | 0.280 lb/in³ |
| Melting Point (approx.) | ≈ 1500 °C | ≈ 2730 °F |
| Modulus of Elasticity | 218 GPa | 31.6 × 10³ ksi |
| Thermal Conductivity (100°C) | 26 W/m·K | 15.0 BTU/h·ft·°F |
| Mean Thermal Expansion (20–300°C) | 11.3 µm/m·°C | 6.3 µin/in·°F |
| Specific Heat | 0.46 J/g·°C | 0.11 BTU/lb·°F |
| Max. Service Temperature | ≈ 650 °C | ≈ 1200 °F |
F91 socket weld fittings as per ASME B16.11 – Class 3000 & 6000 (mm)
| NPS | Socket Bore (B) | Socket Depth (J) min | 90° Elbow / Tee / Cross (A) – 3000 | 90° Elbow / Tee / Cross (A) – 6000 | 45° Elbow (A) – 3000 | 45° Elbow (A) – 6000 |
|---|---|---|---|---|---|---|
| 1/8" | 10.9 | 9.5 | 11.0 | 11.0 | 8.0 | 8.0 |
| 1/4" | 14.3 | 9.5 | 11.0 | 13.5 | 8.0 | 8.0 |
| 3/8" | 17.7 | 9.5 | 13.5 | 15.5 | 8.0 | 11.0 |
| 1/2" | 21.9 | 9.5 | 15.5 | 19.5 | 11.0 | 13.0 |
| 3/4" | 27.3 | 12.5 | 19.5 | 22.5 | 13.0 | 14.0 |
| 1" | 34.0 | 12.5 | 22.5 | 27.0 | 14.0 | 17.0 |
| 1 1/4" | 42.8 | 12.5 | 27.0 | 32.0 | 17.0 | 21.0 |
| 1 1/2" | 48.9 | 12.5 | 32.0 | 38.0 | 21.0 | 25.0 |
| 2" | 61.2 | 16.0 | 38.0 | 41.0 | 25.0 | 28.0 |
| 2 1/2" | 73.9 | 16.0 | 41.0 | – | 28.0 | – |
| 3" | 89.9 | 16.0 | 57.0 | – | 32.0 | – |
| 4" | 115.5 | 19.0 | 66.5 | – | 41.0 | – |
A = Centre to bottom of socket. Class 3000 is used with SCH 80 pipe and Class 6000 with SCH 160 pipe. All dimensions in mm and nominal; tolerances as per ASME B16.11.
Where ASTM A182 F91 forged fittings are used
Main steam and hot reheat drains, vents and instrument tappings.
Header and superheater outlet connections at peak temperature.
Combined-cycle high-pressure superheater and reheater piping.
High-temperature heater and hydroprocessing small-bore lines.
Steam generator auxiliaries and turbine bypass connections.
Cracker and reformer service where creep strength is critical.
Quality you can verify on every heat
Large inventory for fast dispatch
MTC EN 10204 3.1 / 3.2
Positive material identification
Pan-India & export shipping
Quick answers about A182 F91 forged fittings
Get competitive pricing, ready stock and complete documentation.